Product Temperature Curve: Core Evidence for Brazing Furnace Commissioning and Changeover
The furnace temperature setpoint does not equal the actual product temperature, and the temperature profile must be validated according to the product and loading method.
Jinglian Zhongrui Technology Team
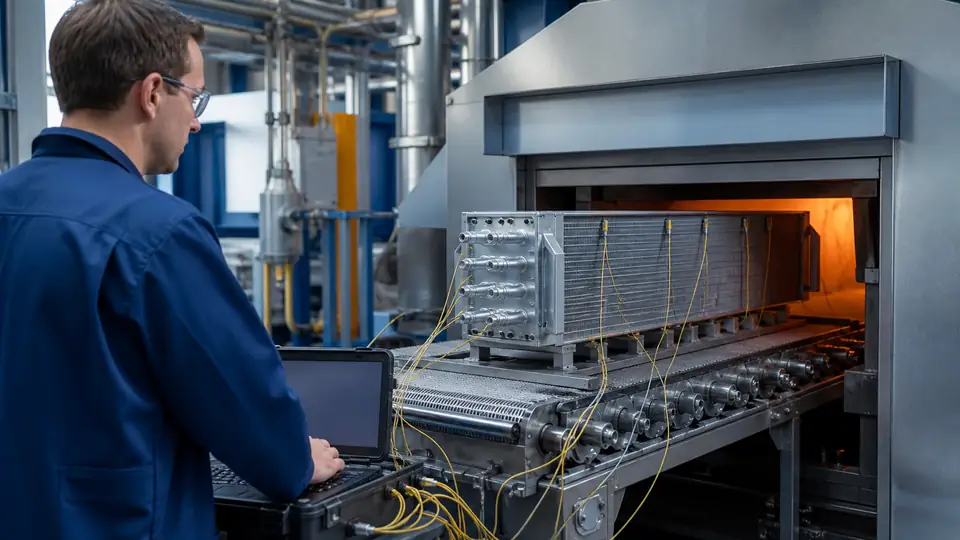
Key Points Under the same furnace temperature program, different quality, structure, placement positions, and loading density will produce different thermal responses. Product temperature measurement is the common language for debugging, model changes, and problem reproduction.
Implementation Focus 1. Select representative measurement points such as thick walls, thin walls, the inlet end, and shaded areas. 2. Fix the thermocouple installation method to reduce contact and radiation errors. 3. Record information on the empty furnace state, chain speed, fans, atmosphere, and loading. 4. Correspond the temperature curves with joint appearance, air tightness, and metallographic results.
Verification and Closed-Loop After major maintenance, cycle changes, or product model changes, the curve should be reconfirmed according to risk.
Project Recommendations During scheme review, input conditions, target values, verification methods, and responsible persons should be recorded in a single traceable document; if changes occur, simultaneously evaluate the impact on design, manufacturing, and delivery.Doing this can transform experience into stable and replicable engineering capability. Further reading: Solvay NOCOLOK Technical Center: https://www.solvay.com/en/brands/nocolok/technical-center Solvay NOCOLOK Technical Data: https://www.solvay.com/en/brands/nocolok/publications